
Editor’s Note: The paper on which this article is based was originally presented at the 46th Annual EOS/ESD Symposium in September 2024. It was subsequently awarded Outstanding Paper (Manufacturing), Best Paper, and Best Student Paper at the 47th Annual EOS/ESD Symposium in September 2025. It is reprinted here with the gracious permission of the EOS/ESD Association, Inc.
In the semiconductor industry, there is currently a growing trend towards Multi-Chip Modules (MCM) and Systems in a Package (SiP). These MCMs and SiPs consist of multiple dies/chiplets, sensors, and often delicate optoelectronic components that have minimal protection against Electrostatic Discharge (ESD). Figure 1 presents a schematic representation of such a MCM, including the internal pins, through silicon vias (TSV) and interposers, that do not have any connection to the outer world once assembled.
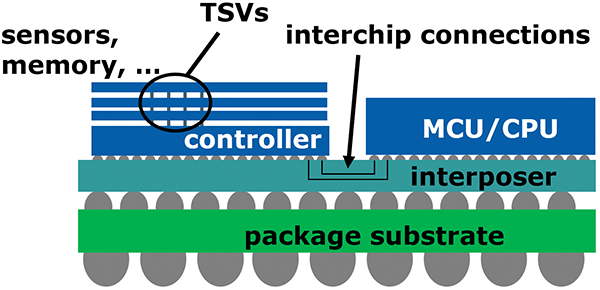
During the assembly of these MCMs, the components may be exposed to ESD stress due to handling. There are methods available to determine the Charged Device Model (CDM) [1] robustness of single devices, such as standard CDM testing or more advanced techniques like capacitively-coupled transmission line pulsing (CC-TLP) [2] [3] [4] [5] [6] [7] or low-impedance contact CDM (LICCDM) [8] [9]. The CC-TLP method allows for highly reproducible stress testing and has demonstrated its correlation with CDM at various levels, including package, wafer, and bare dies. For the CC‑TLP the robustness level is determined by evaluating the measured stress current. This current is then compared to the stress currents measured during a CDM test to obtain the corresponding CDM voltage, which is used to assess the ESD risk in a production environment.
However, there is a lack of available data that correlates the measured voltage in a production machine with the discharge currents that may occur during the production process, such as the pick and place process. This limitation prevents the evaluation of the robustness of a bare die solely based on the determination of the failure current. Publication [10] presents a method on how to correlate the discharge current with the pre-charge voltage based on the package parameters. However, the actual currents occurring during the assembly process, for instance inside a pick and place machine, are currently unknown. This paper proposes a method of how to close this gap by directly measuring the occurring discharge current during the pick and place process. These data provide valuable information about the maximum currents which have to be taken into account during the development stage of the ESD protection.
Section II shows first measurements with a multi‑purpose current monitor designed for detecting secondary discharge during system level ESD testing [11]. Section III follows with the design of a dedicated Discharge Current Sensor (DCS), which can be placed directly into an assembly machine. This DCS is further used in Section IV for the evaluation of discharge currents in a laboratory environment and in a production machine (Sub-sections A and B).
Pre-Test Measurements (II)
First measurements are performed using a current sensor which was previously built for detecting secondary discharge current during system level ESD testing with an ESD gun [11]. Figure 2 shows the measurement setup.
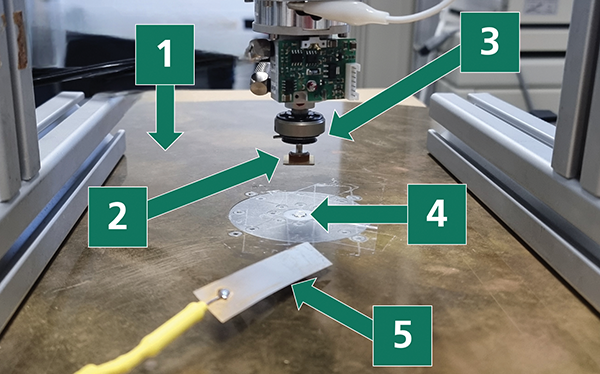
The current sensor (Figure 2, arrow marker 4) is integrated in a large, round ground plane (Figure 2, arrow marker 1) [11]. The current monitor is connected to an oscilloscope to measure the current via a shunt resistor [11], similar to a CDM head. The device under test (DUT) is a fully metallized chip which emulates the worst-case scenario of a die with the highest metallization density (Figure 2, arrow marker 2). A vacuum picking tool as it is used in pick & place machines (Figure 2, arrow marker 3) fixes the DUT. The picking tool allows to move the DUT in Z-direction, touching the current monitor in its lowest position. A charging probe (Figure 2, arrow marker 5) is used to charge the DUT.
To obtain the correct discharge current, it is of importance to charge the DUT at the same Z-height as the discharge occurs, as the capacitance changes with the distance from the ground plane. Therefore, the following test sequence is applied: 1) the DUT is elevated and the current monitor covered with a thin ceramic plate, 2) the charging probe is placed on the ceramic plate and the DUT is lowered in the touchdown position contacting the charging probe (=charging of the DUT), 3) the DUT is elevated again and the ceramic plate is removed, 4) the DUT is lowered in the touchdown position and discharges into the current monitor.
For the first preliminary measurements with the available current sensor used in [11], six positive and negative pre-charge voltage points are chosen to see the tendencies for the discharge currents. The lowest pre-charge voltage starts at 50 V and goes up to 300 V in 50 V steps. Figure 3 shows the absolute peak currents for the given pre-charge voltages. The peak current increases with the pre-charge voltage. However, due to the occurring air discharge, there is a strong variation of the peak current. Moreover, the surface of the current sensor’s electrode is fairly large compared to the size of the DUT, which makes the contact face undefined. This may further increase the variation of the peak currents and emphasize the need for a specialized current sensor.
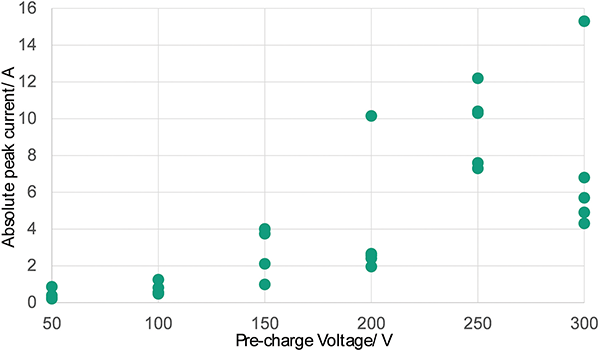
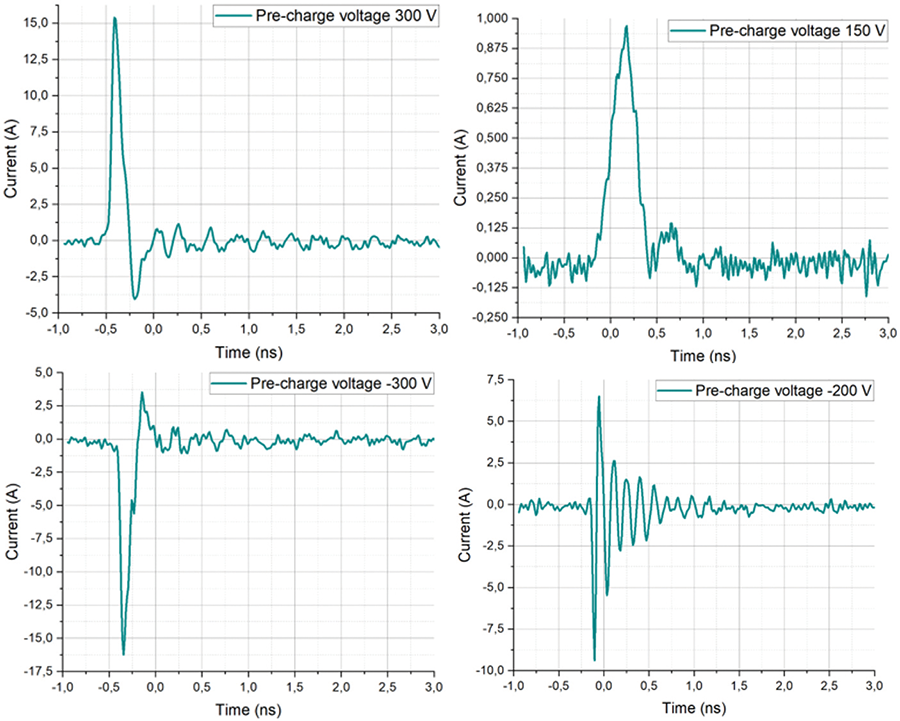
Figure 4 presents a selection of the obtained discharge current waveforms. Overall, the pulse shape is similar to the typical CDM discharge waveform with faster rise times (few ps) and shorter pulse widths (~200 ps). Therefore, it is of importance to use a fast-sampling oscilloscope and a current sensor with a high bandwidth.
Design of the Current Sensor (III)
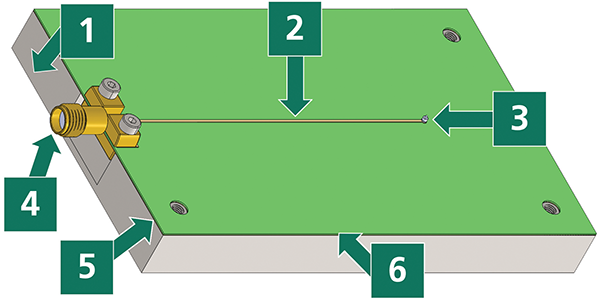
For this purpose, a Discharge Current Sensor (DCS) is designed. The size of the DCS allows it to place it within an assembly machine. It is based on a 50 Ω microstrip line terminated by a miniature pogo pin (Figure 5, arrow marker 3) with a diameter < 2 mm and length < 3.5 mm, to keep the mismatch to 50 Ω as small as possible. Up to 10 resistors of the size 02016 can be placed between the conductor (Figure 5, arrow marker 2) and the ground plane (Figure 5, arrow marker 5). It deploys high frequency thin film resistors and high frequency dielectrics (Figure 5, arrow marker 6) with low dielectric constant variation up to 50 GHz. The metal plate, indicated by arrow marker 1 in Figure 5, is used to stabilize the current sensor. The microstrip line is connected to a 33 GHz bandwidth oscilloscope using a SMA connector (Figure 5, arrow marker 4).
Measurement Results (IV)
In this section, measurements using the DCS are presented. Section A discusses measurements in laboratory using the simplified pick & place head as shown in Figure 2, arrow 3. Section B presents in situ measurement results from a state-of-the-art assembly machine.
Measurements in the Laboratory Environment
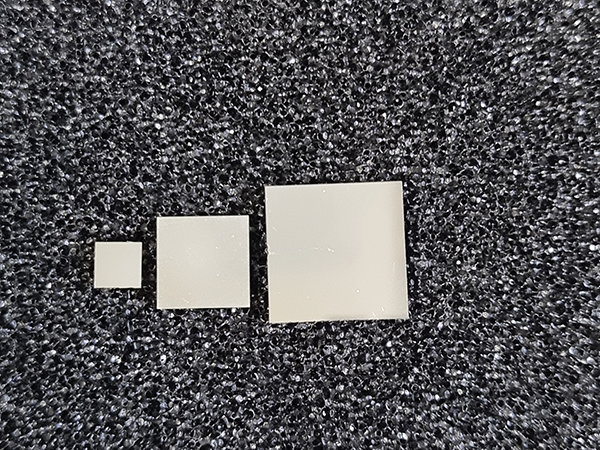
The main goal of the measurements in a laboratory is to gain some first statistical data using the Discharge Current Sensor. Therefore, DUTs of 3 different sizes are employed: 5 mm x 5 mm, 10 mm x 10 mm and 15 mm x 15 mm. Figure 6 presents these fully metallized aluminum dies. Furthermore, 13 positive and negative pre-charge voltage levels are chosen: 4 V, 6 V, 8 V, 10 V, 15 V, 20 V, 25 V, 30 V, 35 V, 40 V, 50 V, 75 V and 100 V. Lower voltages than the standard CDM test condition (TC) levels are selected, as these are realistic values that can occur in a modern production process.
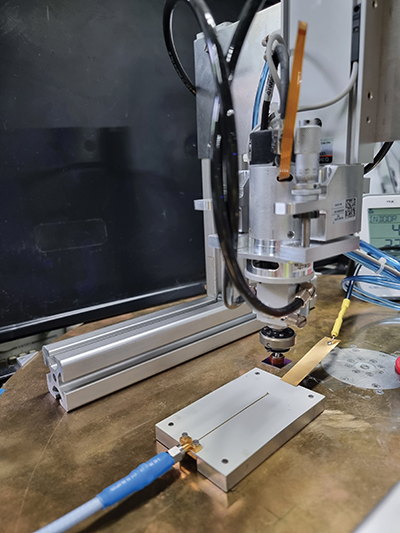
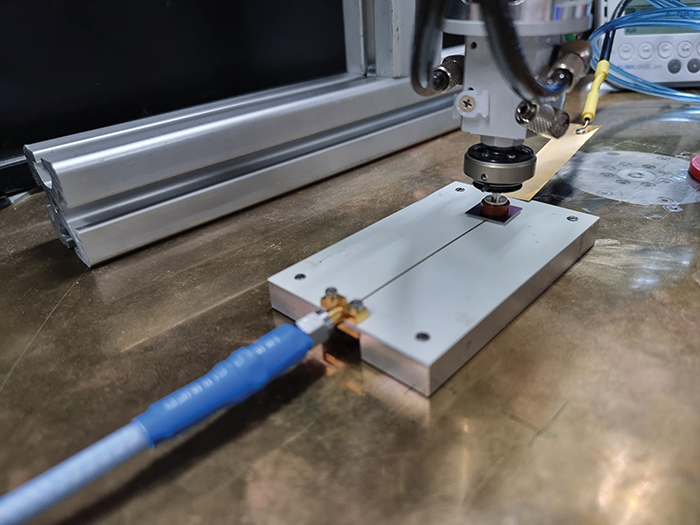
The same method as described in Section II is used for measurements with the Discharge Current Sensor. The DCS is placed below the pick & place head with the miniature pogo pin facing the DUT. The DUT is charged with the charging probe at the same Z-height at which the discharge takes place and finally discharged via the miniature pogo pin into a microstrip line connected to the high bandwidth oscilloscope. Figures 7 and 8 show the measurement setup with the DUT in an elevated position (Figure 7) as well as in the discharge position, when the DUT touches the miniature pogo pin of the DCS (Figure 8).
The ambient temperature and the relative humidity during the discharge test are monitored in the vicinity of the DCS. The relative humidity fluctuated between 20 % and 24 %, while the temperature on the first day of the discharge tests (DUTs: 5 mm x 5 mm and 10 mm x 10 mm) was 27 °C to 27.3 °C and 23.5 °C to 24 °C on day two (DUT: 15 mm x 15 mm).
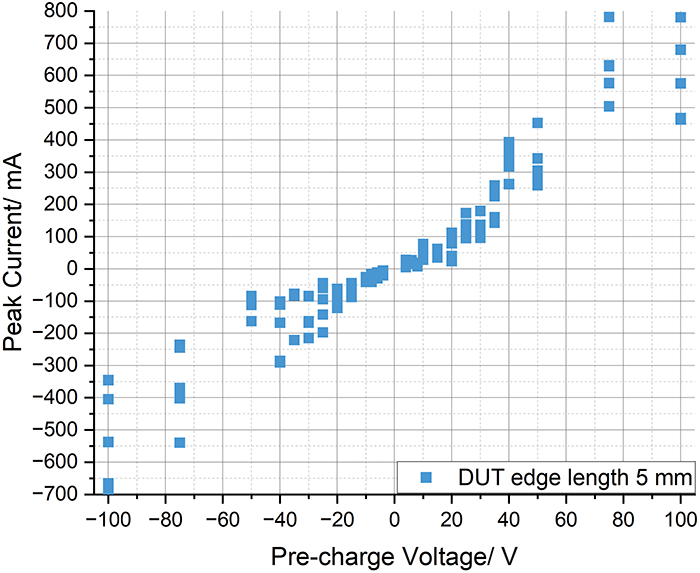
Figure 9 depicts the peak values of the discharge current for the smallest DUT with an edge length of 5 mm. 5 peak current values are listed for each of the 26 voltage levels.
Figures 10 and 11 refer to the metallized die with a size of 10 mm x 10 mm. While Figure 10 presents its peak current distribution, Figure 11 shows a typical discharge current waveform for a pre-charge voltage of 6 V. This curve confirms the results obtained in Section II, proving the discharge currents captured with DCS to be similar to those of the CDM, but with much narrower pulse widths and very fast rise times. In Figure 11, the pulse width at half maximum equals 66.5 ps with a 10 % to 90 % rise time of 40 ps.
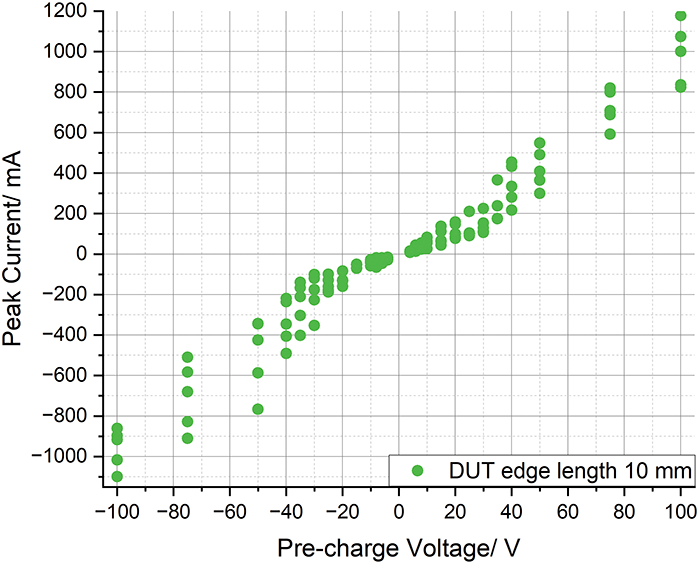
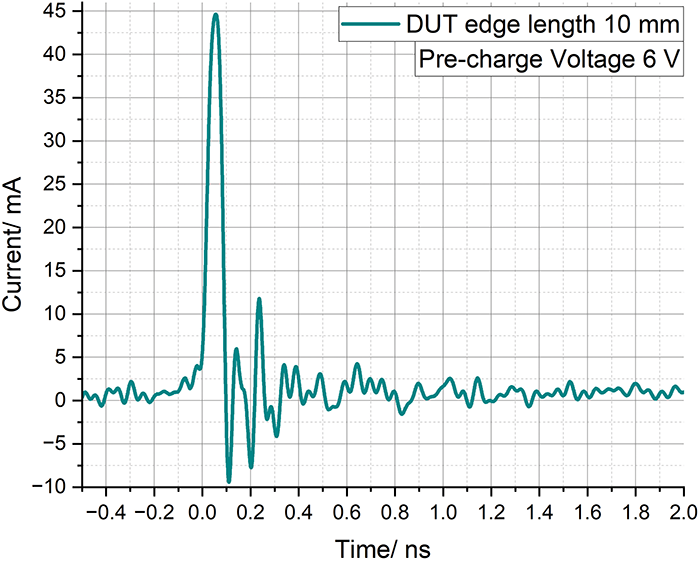
Figure 12 displays the peak current values of the DUT with an edge length of 15 mm, which is the largest one used during this study.
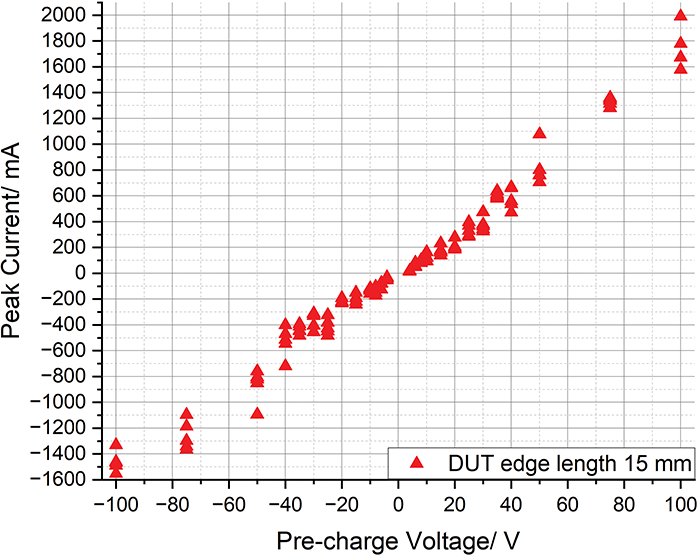
The variation of the peak current values increases with increasing pre-charge voltage. This can be explained by different discharge mechanisms taking place at different voltage levels. At higher voltages, air discharge occurs which is triggered by an avalanche effect. This strongly depends on the environmental conditions like the relative humidity and air pressure and yields higher variation of the peak currents. At lower voltages, field emission is the dominant discharge mechanism. It strongly depends on the quality of the surface of the discharge electrodes. Since the deposited aluminum layer of the DUT shows a low roughness, the field emission ensures more reproducible pulses. This becomes more evident if the peak current is referenced to the pre charge voltage (Figure 13).
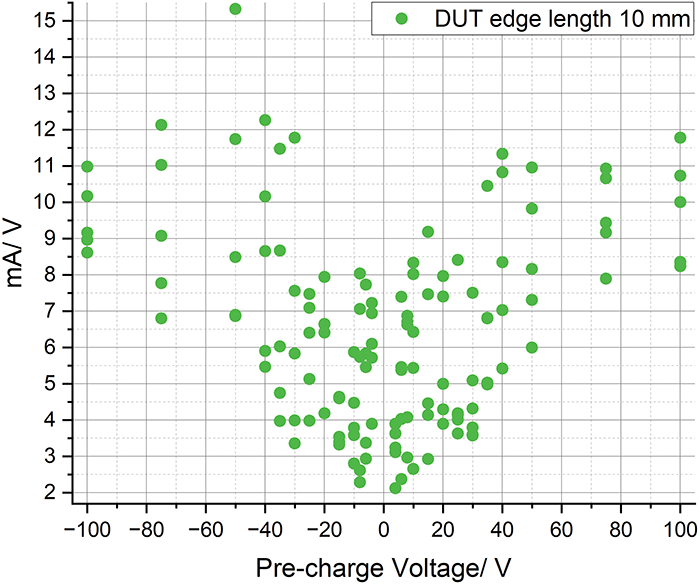
The data in Figure 13 show higher current values per Volt for pre-charge voltages higher than 30 V. The mean value in this region is in the range of 10 mA/ V. For pre-charge voltages below 30 V, the mean value is in the range of 5 mA/ V. This supports the hypothesis of different discharge mechanisms for the different pre‑charge voltage regions.
Voltages below ± 30 V are of special interest in the field of assembly machines, since it is fairly complicated to fully control the charging of all parts involved in an automated assembly process at all times. Therefore, Figure 14 shows the distribution of peak currents for all 3 evaluated metallized dies: 5 mm x 5 mm (Figure 14, blue squares), 10 mm x 10 mm (Figure 14, green circles) and 15 mm x 15 mm (Figure 14, red triangles). Moreover, lines of best fit in corresponding colors are added to simplify the visualization and readout of the data. The small difference between the peak currents of the DUTs with 5 mm and 10 mm edge length may be caused by the rather high variations of peak currents in both datasets.
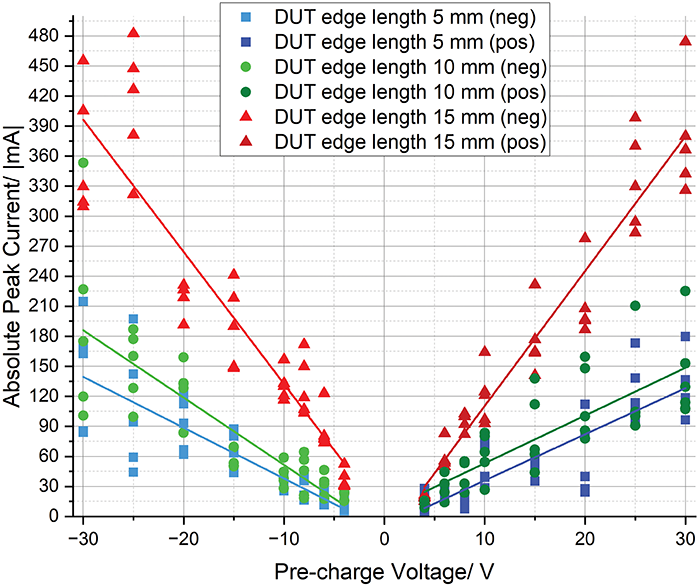
The results show that the peak discharge currents are lower compared to the expected interpolated values of the CDM. For the small verification coin, which has a smaller area than the 10 mm x 10 mm die, the interpolated values would be at 60 mA at 4 V and 440 mA at 30 V.
Measurements in Pick & Place Machine
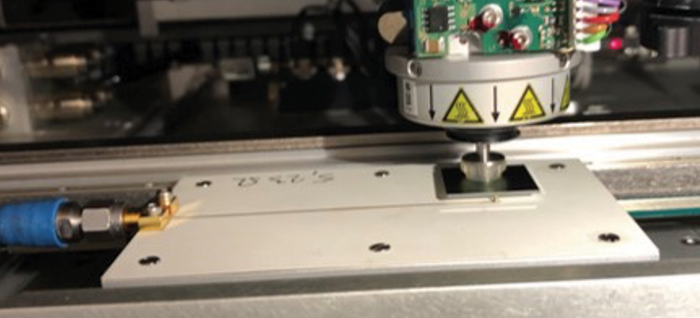
The tests inside the pick & place machine consist of picking fully metallized dies with an edge length of 10 mm from a blue tape carrier and placing them on the pogo pin of the DCS. Figure 15 shows the current probe mounted inside a state-of-the-art assembly machine with the die on top of the pogo pin. In order to emulate the worst-case scenario, the setup employs a fully metallized die and an isolated picking tool.
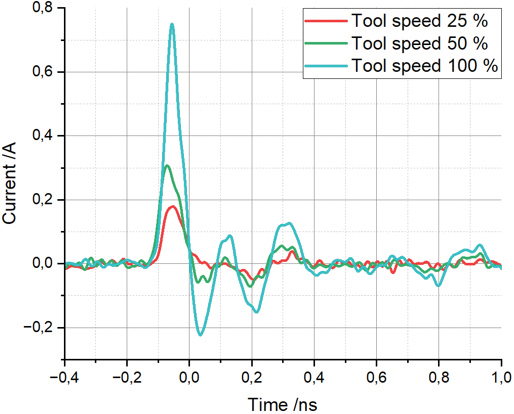
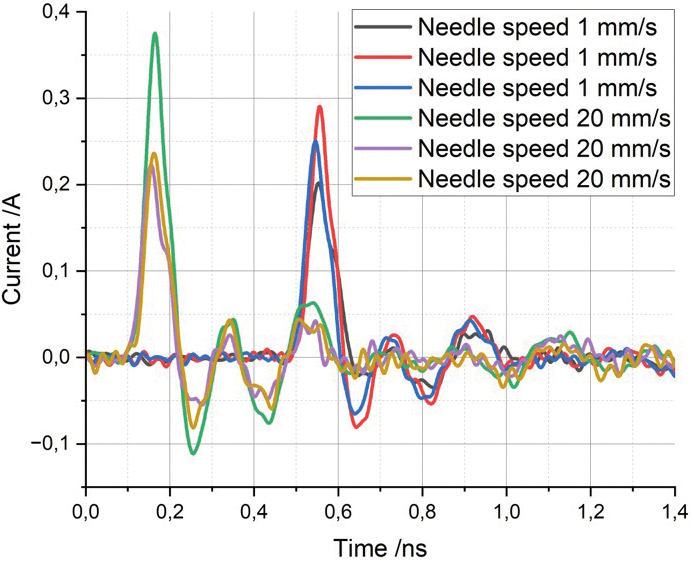
The tool speed, needle speed and moving path of the picking tool are varied to examine their influence on the measured discharge current. Figure 16 shows that the discharge current increases with increasing tool speed.
Since the DUTs are placed on a blue foil, the assembly machine stamps the DUT out using needles penetrating the blue foil, to overcome its adhesive force. The needle speed defines the velocity at which the needles puncture through the carrier foil. The needle speed does not have any influence on the velocity at which the die is picked from the blue tape by the tool. Figure 17 demonstrates that there is no clear correlation between the needle speed and the peak current.
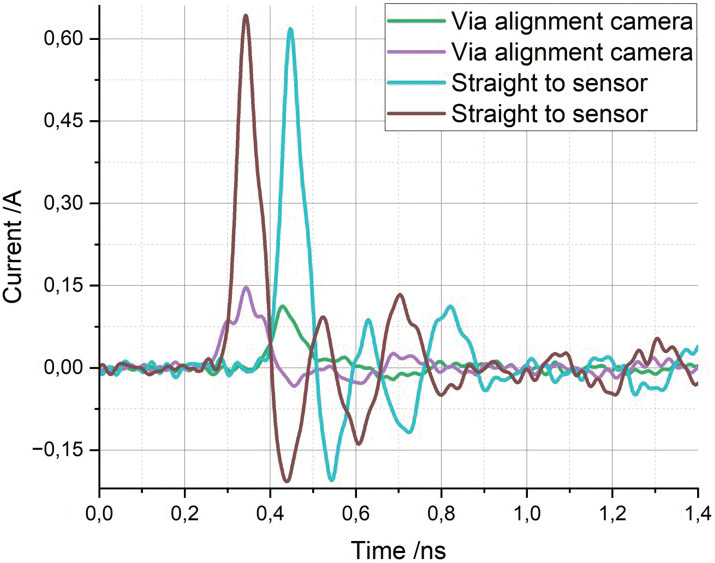
Finally, Figure 18 compares the discharge currents for two moving paths of the picking tool: via an alignment camera (green and lilac curves) and directly to the sensor (turquoise and brown curves). On the direct path, there is less time between picking of the die and placing it on the pogo pin of the DCS, leading to higher discharge currents. Consequently, the moving path via an alignment camera introduces more time between the charging of the DUT and the discharge to the sensor and thus lowers the ESD current.
Conclusion and Outlook (V)
This paper presents a current sensor which can be employed directly in an assembly machine for in situ ESD current measurements. Experiments in a simplified laboratory environment help to link voltage levels to measured discharge currents and show some first statistical data for three different DUT sizes. The measured discharge curves are not compliant with the JS-002 standard [1] as they display faster rise times and shorter pulse widths. Furthermore, measurements in a pick & place machine under worst-case conditions are presented showing the increased ESD risk for faster tool speeds and shorter time between the picking (=charging) and placing (=discharging) of the die. The current sensor can be used for verification and improvement of production machines as well as comparison of different production machines. Moreover, the presented method has the potential to better understand and estimate the risks occurring during the assembly process. The MCMs and SiP designers may profit from these (and future) data to tailor the ESD protection exactly to the requirements.
As an outlook, more statistical data should be collected. For this purpose, an automated measurement setup is required. A re-designed Discharge Current Sensor, which will speed up the measurements, is already in the development stage.
Acknowledgements
The authors thank Marko Simicic (imec) for his patience and valuable feedback. Furthermore, we would like to thank Kai Esmark (Infineon Technologies) for fruitful discussions.
This project was partially funded by the Silicon Valley Community Foundation.
References
- ESDA/JEDEC Joint Standard ANSI/ESDA/JEDEC JS-002-2022 Charged Device Model (CDM) – Device Level.
- ANSI/ESD SP5.3.4-2022 ESD Association Standard Practice for Electrostatic Discharge Sensitivity Testing – Capacitively Coupled – Transmission Line Pulsing as an Alternative CDM Characterization Method.
- H. Wolf, H. Gieser, W. Stadler, W. Wilkening, “Capacitively Coupled Transmission Line Pulsing CC-TLP – A Traceable and Reproducible Stress Method in the CDM-Domain,” Journal of Microelectronics Reliability, Elsevier, volume 45, no. 2, 2005, pp. 279-285.
- H. Wolf, H. Gieser, K. Bock, A. Jahanzeb, C. Duvvury, and Y.-Y. Lin, “Capacitive coupled TLP (CC-TLP) and the correlation with the CDM,” 2009 31st Electrical Overstress/Electrostatic Discharge Symposium (EOS/ESD), Anaheim, CA, USA, 2009.
- K. Esmark, R. Gärtner, S. Seidl, F. zur Nieden, H. Wolf, H. Gieser, “Using CC-TLP to get a CDM Robustness Value,” 2015 37th Annual EOS/ESD Symposium (EOS/ESD), Reno, NV, USA, 2015.
- J. Weber, K. T. Kaschani, H. A. Gieser, H. Wolf, L. Maurer, N. Famulok, R. Moser, K. Rajagopal, M. Sellmayer, A. Sharma, and H. Tamm, “Correlation study of different CDM testers and CC-TLP,” EOS/ESD Symposium Proc. 2017, Tucson, AZ, USA.
- J. Weber, R. Fung, R. Wong, H. Wolf, H. A. Gieser, L. Maurer, “Stress current slew rate sensitivity of an ultra-highspeed interface IC,” IEEE Transactions on Device and Materials Reliability, vol. 19, issue 4, November 2019.
- N. Jack, B. Carn, and J. Morris, “Toward Standardization of Low Impedance Contact CDM,” 2019 41st Annual EOS/ESD Symposium (EOS/ESD), Riverside, CA, USA, 2019.
- M. Simicic, W.-M. Wu, N. Jack, S. Tamura, Y. Shimada, M. Sawada, S.-H. Chen, “Optimization of Wafer-Level Low-Impedance Contact CDM Testers,” in 2020 42nd Electrical Overstress/Electrostatic Discharge Symposium (EOS/ESD), Reno, NV, USA, 2020.
- L. Zeitlhoefler, T. Lutz, F. Zur Nieden, K. Esmark and R. Gaertner, “Voltage to Current Correlation for CDM Testing,” 2023 45th Annual EOS/ESD Symposium (EOS/ESD), Riverside, CA, USA, 2023.
- H. Wolf, H. Gieser, “Secondary discharge – A potential risk during system level ESD testing,” 2015 37th Electrical Overstress/Electrostatic Discharge Symposium (EOS/ESD), Reno, NV, USA, 2015.
